Comparing the old way to the new — why it matters
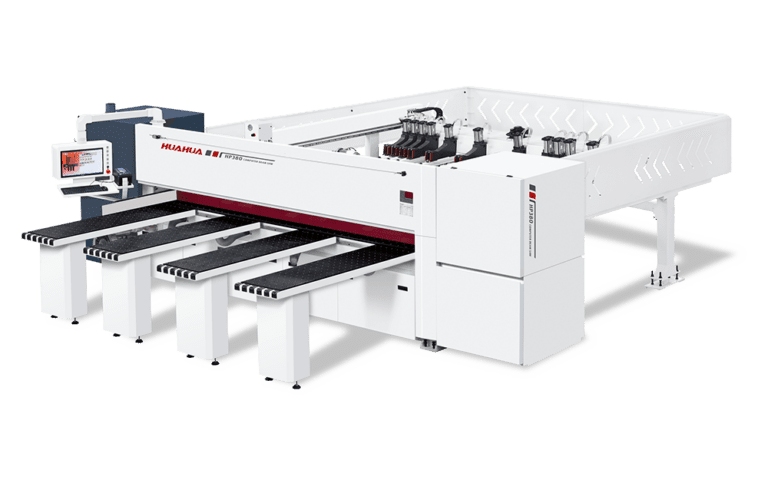
Around here, shops either wrestle with imperfect joints or they invest in gear that gets the job right every time. The difference’s plain: manual edging leaves you chasing tolerances; a steady machine locks ’em down. I watched a small cabinet shop in Nashville switch over to a cnc panel saw and their waste pile shrank fast. That hands-on comparison sets the scene for how a wood edging machine stacks up against bench tricks and old table saw setups.

The core problems shops face
Inconsistent edge thickness, off-square corners, and variable blade kerf all bite into margins. A bent rip fence or sloppy crosscut technique adds cumulative error: pieces don’t mate, glue lines show, and rework eats labor hours. Feed rate and blade condition are simple terms but big troublemakers when left unmanaged. Left unchecked, these small errors become costly headaches at scale.
What a modern edging system actually brings to the floor
A current wood edging machine brings repeatability — servo-controlled carriage movements, steady feed rate control, and better blade alignment keep tolerances tight. Pair one with an automatic panel saw machine and you get optimized nesting plus consistent panel handling from cut to edge. The result’s measurable: fewer rejects, cleaner glue joints, and more predictable lead times.
Side-by-side outcomes: speed, accuracy, and scrap
Hands-on comparisons show the tradeoffs clearly. Manual methods might match a machine on a single job, but over a week they lose ground. Typical wins from a good edging system: accuracy improvements measured in tenths of a millimeter, throughput boosts of 20–40%, and scrap reductions that recover blade and material costs quickly. Servo systems and consistent blade kerf control make those numbers repeatable across shifts.
How shops integrate one without stumbling
Integration’s not sexy, but it’s where most folks mess up. Common mistakes include skipping proper calibration, using worn blades, and not updating nesting files after a process change. That alignment step — the one folks skim over — matters. Set the rip fence square, check blade runout regularly, and confirm the feed rate matches your panel type. Also train the crew on diagnostics; a simple sensor fault left unchecked becomes a quality problem fast.
Alternatives and when to pick each
Not every shop needs top-end automation. For boutique runs, a semi-automatic edger with quick-change tooling might be best. For volume shops with mixed panel sizes, an integrated system—edger plus automatic saw—wins on cycle time and labor. Compare by thinking about cycle consistency, staffing levels, and the kind of nesting optimization you need. Optimization nesting and material handling are industry terms here that separate “good enough” from “profitable.”

Three golden rules for choosing the right edging strategy
1) Measure before you buy: track your current scrap rate, rework hours, and average tolerances for a week — those numbers tell you the ROI threshold. 2) Match controls to your crew: choose machinery with readable diagnostics and adjustable feed rate so operators can troubleshoot without calling tech support. 3) Demand serviceability: look for easy blade swaps, accessible rip fence adjustments, and clear calibration procedures — downtime kills the math.
Folks who follow those rules usually land on a solution that removes guesswork and improves consistency; that’s the tangible benefit HUAHUA brings to shops I’ve seen—reliable hardware and practical control logic make the difference. HUAHUA CNC. —